Construction and properties
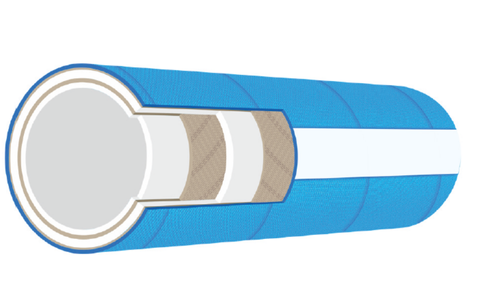
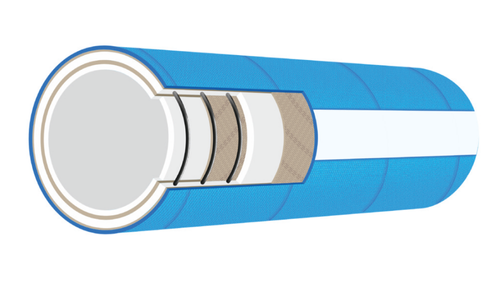
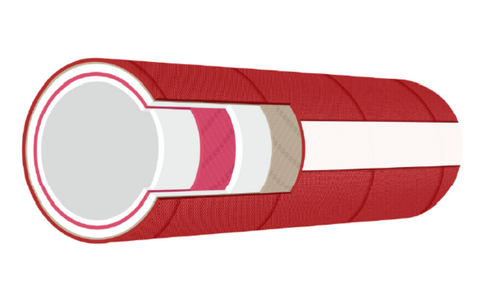
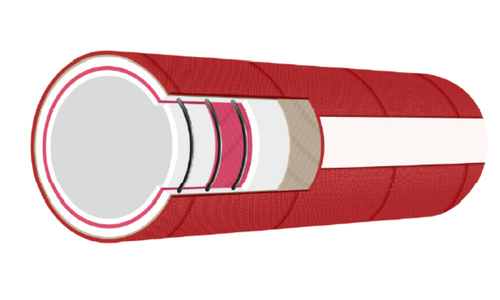
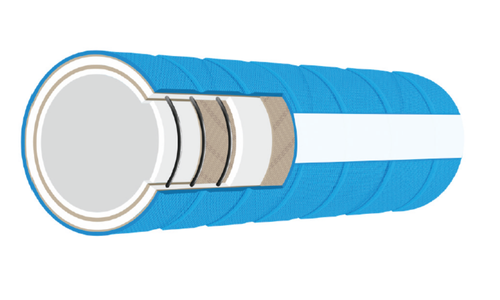
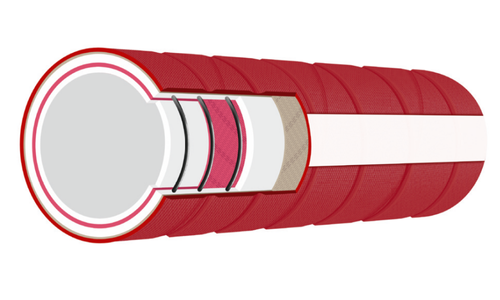
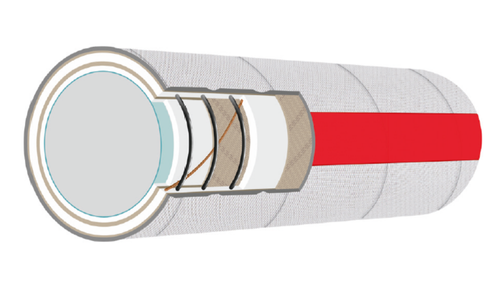
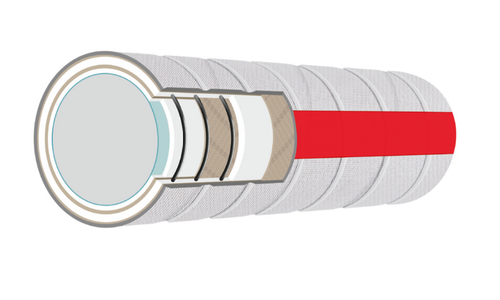
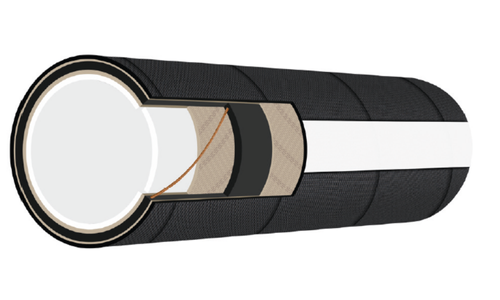
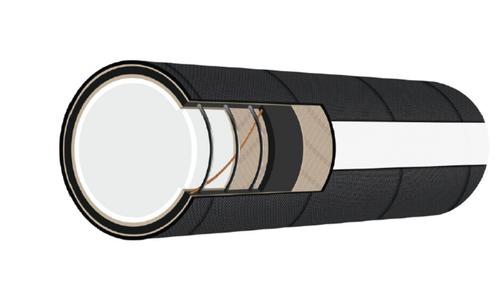
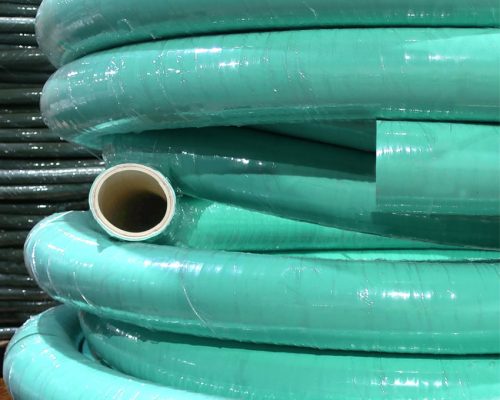
Rubber hoses for food products are manufactured from special, certified rubber that is safe for food contact. The inner layer of the hose is smooth, odorless, and does not release any substances that could alter the taste, smell, or composition of the transported product. This layer is also resistant to fats, acids, sugar solutions, alcohol, and other food components.
The reinforcement layer provides strength and allows the hose to be used in both low- and high-pressure systems. The outer layer is resistant to temperature fluctuations, mechanical damage, and disinfectants used for cleaning food production lines.
Some hoses have additional properties, such as resistance to heat, steam sterilization, or higher vacuum levels, allowing them to be used in particularly demanding technological systems.
Areas of application
Rubber hoses for food products are used in various production, processing, and packaging lines. They are most commonly applied in the following areas:
In the dairy industry – for milk, whey, and other liquid products
In the beverage industry – for water, soft drinks, beer, wine, juices, and syrups
For transporting oils and fats
For supplying sugar solutions, glazes, concentrates, and other viscous products
In food production lines where hygienic product transfer is required
In the pharmaceutical and cosmetic industries, where an exceptional level of cleanliness is required
In the agricultural sector for supplying liquid feed and supplements
Due to their hygienic properties and resistance to cleaning agents, these hoses are easy to maintain, allowing efficient upkeep of high production hygiene standards.
Why choose a rubber hose for food products?
Main advantages:
Hygiene and safety – certified materials suitable for food contact.
Neutrality – the hose does not alter the product’s taste, smell, or color.
Resistance to fats and acids – suitable for various types of food products.
Durability – resistant to disinfection, temperature changes, and intensive use.
Versatility – adaptable to many food processing applications.
Rubber hoses for food products are an essential component of any production or processing line where safe, clean, and reliable product transport is required. They ensure a high level of hygiene, efficiency, and help maintain consistent production quality across all processes.