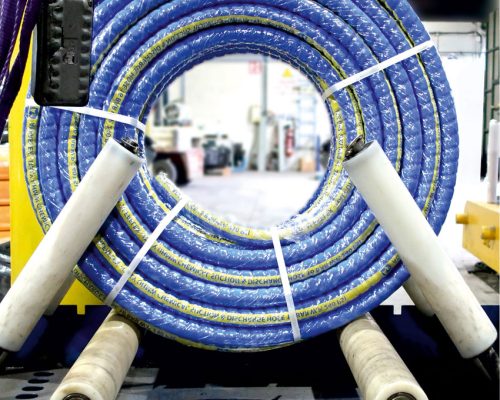
Construction and properties
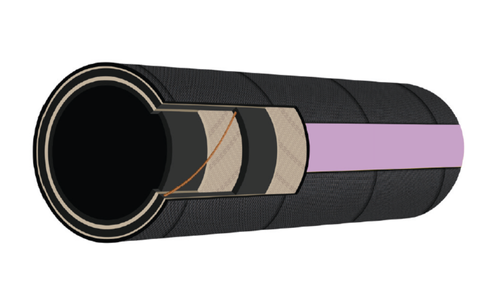
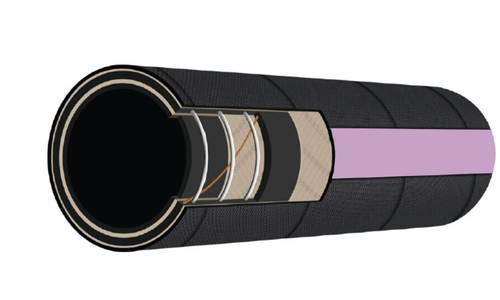
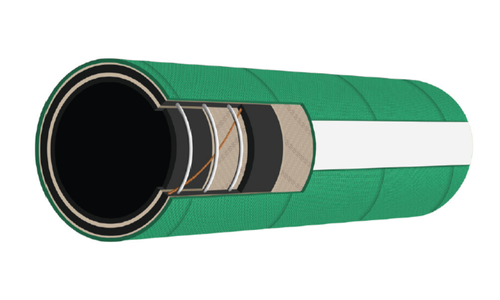
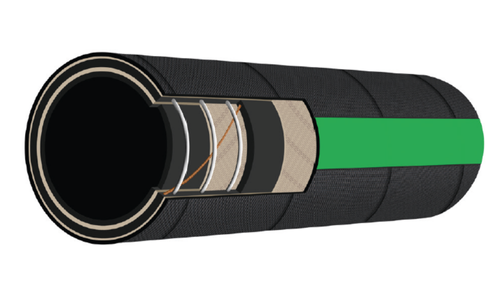
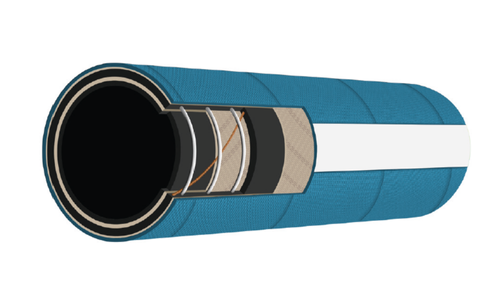
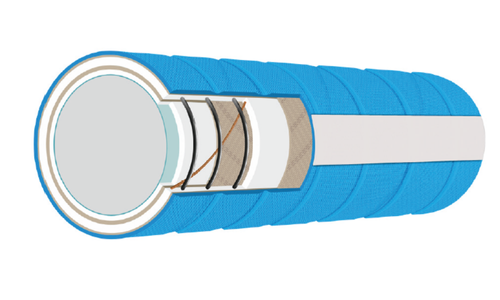
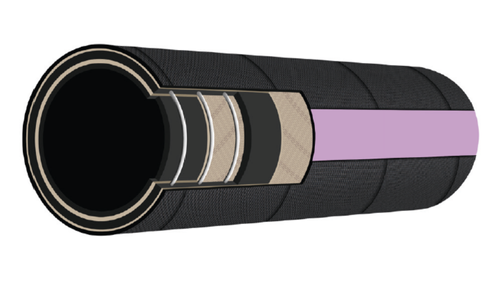
Rubber hoses for chemical applications are manufactured from specialized rubber compounds such as EPDM, nitrile rubber (NBR), Viton (FKM), neoprene, and other synthetic polymers with high chemical resistance. The inner layer of the hose is resistant to acids, alkalis, solvents, and aggressive liquids, preventing any reaction between the conveyed medium and the hose material that could damage either the hose or the product being transported.
The reinforcement layer provides the hose with strength and pressure resistance. It can be made of textile, synthetic fibers, or steel reinforcement. The outer layer is resistant to UV radiation, environmental influences, temperature fluctuations, and mechanical damage. This is particularly important in industrial environments where hoses are often used intensively.
Some professional chemical hoses are equipped with an antistatic layer, which prevents the buildup of static electricity and reduces the risk of explosion when working with flammable chemicals.
Applications
Rubber hoses for chemical applications are used across a wide range of industries, as many processes require the transfer of both mild and highly aggressive liquids. Typical applications include:
Transportation of chemicals in manufacturing plants
Agricultural sprayers (for fertilizers, pesticides, and herbicides)
Supply of cleaning and disinfecting solutions used in the food industry
Laboratory processes and experimental systems
Oil, gas, and industrial equipment
Pharmaceutical manufacturing and processing
Industrial laundries and cleaning systems
Water treatment and wastewater processing equipment
Due to their resistance and safety, these hoses are suitable for both low- and high-pressure systems, as well as for transporting aggressive and neutral liquids.
Why choose a rubber hose for chemical applications?
Key advantages:
Chemical resistance – resistant to acids, solvents, alkalis, and other aggressive compounds
Long service life – maintains structure and performance even under intensive use
Safety – protects against leaks, chemical reactions, and potential system damage
Resistance to temperature and pressure – suitable for a wide range of industrial and technological systems
Versatility – applicable from laboratory environments to large-scale production facilities
Rubber hoses for chemical applications are an essential component wherever safe, reliable, and chemically resistant fluid transfer is required. They are designed to ensure maximum safety, minimize the risk of failures, and provide long service life even under demanding operating conditions.